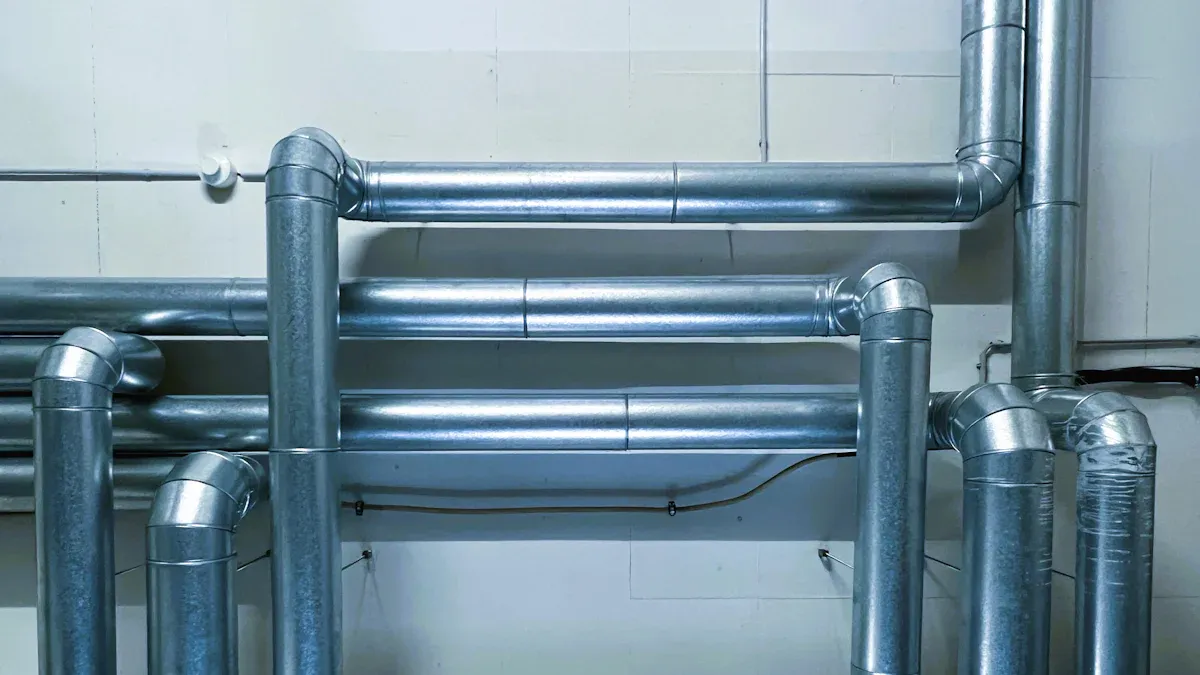
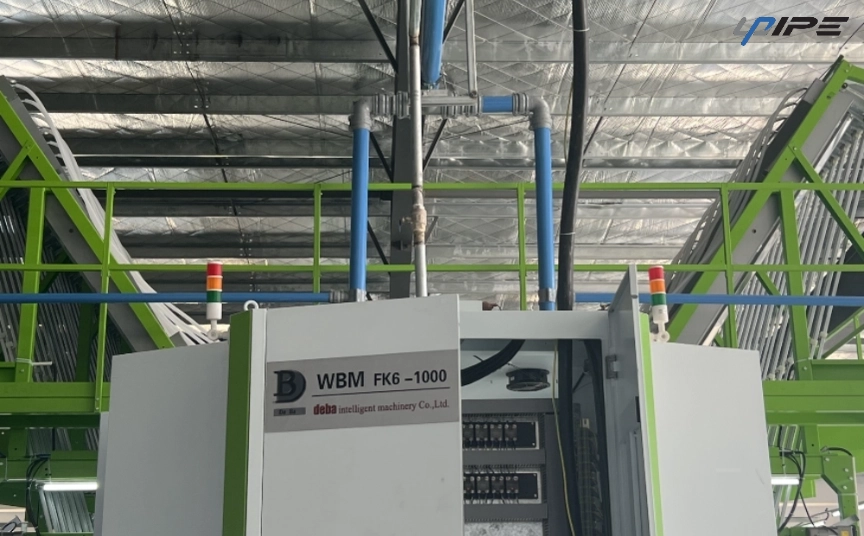
Fast-install aluminum compressed air pipes go together in a clear order: you get tools and materials ready, cut and deburr the pipe, mark the layout, insert the fittings, secure the run, and pressure-test for leaks. Each stage builds on the one before it.
The process does away with welding and threading completely. That change cuts installation time by up to 85% compared with traditional steel or copper piping, and the finished system still stays tight against leaks.
The system can be installed up to 85% faster than traditional piping, using simple tools with no welding, gluing, or crimping needed.
You only need a small set of tools for this job. A pipe cutter does most of the work. A rotary cutter is not always needed, and PVC cutters work fine for 3/4-inch lines. Add a deburring tool and a chamfer tool to clean both ends of each cut. A marker and a tape measure help you mark lengths and cutting points correctly. Keep a wrench close by for the final tightening.
Safety gear is just as important as the tools. Wear gloves to keep your hands safe from sharp cut edges. Put on safety glasses before you cut or deburr, since aluminum shavings fly off easily. Good lighting helps you find burrs and check that each pipe sits fully in its fitting.
Pipes, fittings, and accessories
The Upipe Aluminum Pipe System shows what a fast-install kit looks like. Every pipe is made of pure aluminum with no recycled material. The ends come already cut to size, and a thicker wall design is used on all models. Pipes of DN40 and above come with pre-treated raised rings, which save time on site prep. Sealed packaging with a non-woven fabric lining and outer plastic seal keeps dirt out.
Specification
Detail
Material purity
Pure aluminum, no recycled material
Wall thickness
Thickened wall design on every model
Pre-treated raised rings
Fitted on DN40 and above
The fittings finish off the system. Push-to-connect connectors, tees, and elbows snap onto the pipe with no welding or threading. Quick drops have reinforcement ribs to handle stress imbalance, and passive locking accessories are made of high-strength materials. Built-in aluminum alloy ball valves last a long time in service, and every pipe clamp comes with anti-vibration features. Aluminum works well for fast, low-maintenance industrial compressed air jobs, and this kit gives you everything for a complete run.
Installing aluminum compressed air pipes step by step
Measure the pipe to length first. Mark the cutting location with a marking tool, then work through the cut in a fixed order:
Place the pipe in the pipe cutter, position the blade onto the pipe, then rotate the cutter around the pipe while gently tightening the wheel.
Chamfer the outer edges of the pipe.
Deburr the inner end of the pipe.
Trace the connection indicator with the marking tool.
A combination end-deburring tool saves time here. It removes inside and outside burrs and cuts the chamfer in one pass. Choose tooling that produces a consistent 30° to 45° chamfer on both edges. That angle acts as a lead-in for O-rings and seals. Aluminum forms soft, stringy burrs, so use sharp tools with positive rake angles and a kerosene-based lubricant to stop the metal from smearing. Dull tools push the burr instead of cutting it, and edge quality drops fast.
Respect chamfering limits: over-chamfering weakens the tube's structural integrity and can crack or split under bend load. Target a chamfer depth at or below half the wall thickness, and use a depth gauge or adjustable collar to avoid over-cutting.
Clean off all shavings after deburring. Inside burrs can block fittings and cut seals, so a brief inside pass prevents long troubleshooting later. Light deburring beats aggressive grinding on most aluminum tube work. Add a little oil to the tube before insertion.
Inserting fittings and securing connections
Push the pipe into the connector up to the connection mark. Confirm the pipe sits fully seated, then engage the passive locking accessory. The foolproof, multi-surface sealing design removes guesswork from this step. Imported sealing rubber resists vibration and improper installation, so the joint holds tight even on a busy plant floor.
Space and mount anti-vibration pipe clamps along the run next. Plan clamp spacing before you cut any pipe, since a supported line vibrates less and leaks less. The gooseneck design on quick drops keeps condensate from flowing down into the pipes. That detail protects your equipment downstream and keeps moisture out of the air stream. Quick drops arrive on demand and ready to use, which saves production time on aluminum compressed air pipes.
Check every joint by hand before you move on. A firm tug on the pipe confirms the lock is engaged. Then run your eye along the line and look for gaps at the fitting shoulders.
A pressure test proves your work before the system goes into service. Start by isolating the new section from the rest of the plant. Close the valves that connect it to live air lines. This step keeps the test honest and protects other equipment.
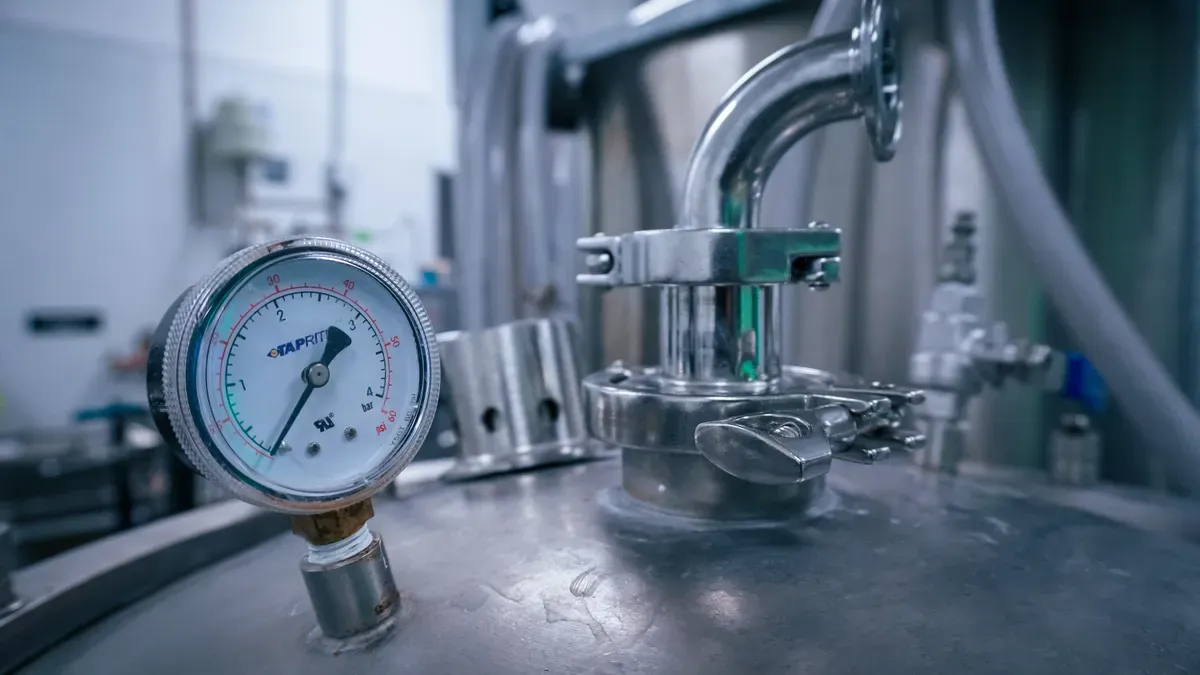
Next, pressurize the isolated section to the system rating. Bring the pressure up slowly. A sudden rush of air can shift a fitting that was not fully seated. Watch the gauge as the pressure climbs.
Hold the section at full pressure for a set period. Walk the entire run during the hold. Check every joint, fitting, and quick drop. Brush leak-detection fluid on each connection and watch for bubbles. Bubbles mean escaping air. A pressure gauge that drops during the hold tells you the same story.
Never skip the hold period. A joint that looks tight at low pressure can weep at full working pressure.
Mark any suspect joint with a marker. Fix it after you release the pressure. Never tighten a fitting on a pressurized line.
Common leak points and fixes
Most leaks trace back to a short list of causes. Check these points first:
Improperly seated pipes. The pipe did not reach the connection mark. Fix: release the lock, push the pipe in until it meets the mark, and re-engage the lock.
Missing or damaged O-rings. The seal is absent or torn. Fix: replace the O-ring with the correct size and inspect the groove for debris.
Loose locking accessories. The passive lock is not fully engaged. Fix: seat the lock by hand and confirm it clicks or seats flush.
Unclamped vibration-prone runs. The line moves under pressure and works the joint loose. Fix: add anti-vibration pipe clamps at the planned spacing.
Work through this list before you suspect anything else. These four causes explain most failures on aluminum compressed air pipes. A firm tug on each pipe confirms the seat. A close look at each O-ring confirms the seal. A hand check on each lock confirms the engagement. A shake test on the run confirms the clamps.
Repressurize after each fix and repeat the hold. Log the final result for your maintenance records. A clean pressure test gives you a baseline for future checks.
Tips for efficient installation
Planning the layout and routing
Sketch the full run before you cut a single pipe. A simple drawing shows every drop point, valve, and bend. Mark where each quick drop goes. Quick drops arrive on demand and ready to use, so you can place them exactly where your equipment needs air.
Plan your clamp spacing on the same sketch. A supported line vibrates less and holds its joints tighter. Route the main line as a loop where possible. A loop shortens airflow paths and keeps pressure steady at distant endpoints. Avoid unnecessary vertical climbs and sharp bends. Each extra bend adds turbulence and pressure loss. Aluminum helps here, since its smooth interior reduces friction loss and turbulence across the network.
Time-saving techniques
Batch your cuts. Measure and cut every pipe for one zone in a single pass, then deburr them together. Grouping these tasks saves repeated tool setup and keeps your rhythm steady.
Keep fittings organized by size in labeled bins. You will grab the right connector on the first try instead of hunting through a pile. On DN40 and above, the pre-treated raised rings skip on-site prep work entirely. Stage materials along the route before assembly begins. Carry pipes, fittings, and clamps to each zone in one trip, then work outward from the compressor.
A few habits pay off across the whole job:
Cut and deburr in batches per zone.
Sort fittings by size before you start.
Use pre-treated raised rings on DN40+ pipe.
Stage materials along the route.
These steps shave minutes off each connection, and the savings add up across a full run.
You now have the full order of steps for a fast-install aluminum compressed air pipe job: get tools and materials ready, cut and deburr each length, insert the fittings, secure the run with clamps, and pressure-test every joint. If you follow each step correctly, fast installation technology gives you both speed and reliability. Systems like Upipe help you install faster and need less maintenance.
Plan the layout before you cut. Use sharp cutters, deburring tools, and the right safety gear. Always pressure-test before the system goes into service. A clean test protects your equipment and your production time. Installing aluminum compressed air pipes the right way pays off for years through steady efficiency and low maintenance.
FAQ
Do I need welding or threading tools for this system?
No. The push-to-connect design removes both steps. You cut the pipe, deburr the ends, and push each length into its fitting until it reaches the connection mark. A pipe cutter, deburring tool, marker, and wrench cover the whole job. That is why the process saves so much time over steel or copper.
How do I know a pipe is fully seated in its fitting?
Push the pipe in until it meets the connection mark. Then engage the passive locking accessory and give the pipe a firm tug. The foolproof, multi-surface sealing design and the imported sealing rubber resist vibration and improper installation. A seated pipe will not pull free under a hand check.
Can I install the pipe near vibrating equipment?
Yes. Mount anti-vibration pipe clamps along the run at your planned spacing. The clamps hold the line steady and keep vibration from working joints loose. Plan that spacing before you cut any pipe. A supported line vibrates less and leaks less over time.
What should I check first if a joint leaks during the pressure test?
Release the pressure before you touch anything. Then check four things in order:
The pipe may not have reached the connection mark.
The O-ring may be missing or damaged.
The locking accessory may not be fully engaged.
The run may need more anti-vibration clamps.
Fix the cause, then repressurize and repeat the hold.
Does the pipe need special prep on larger sizes?
Not on DN40 and above. Those pipes arrive with pre-treated raised rings, so you skip that prep step on site. Every Upipe pipe is pure aluminum with no recycled material and a thickened wall. Sealed packaging keeps the ends clean until you open them.
This website uses cookies to provide you with a safer and more personal experience. By accepting, you agree to the Cookie Policy and the use of cookies for advertising and analytics purposes.